Hydraulic Cylinder Service
Hydraulic ram failure halts critical cargo loading and steering gear operation. At our Tuzla machine shop, we recondition cylinders up to 6 meters length with precision honing, rod straightening, hard chrome plating, and marine PTFE seal packages.
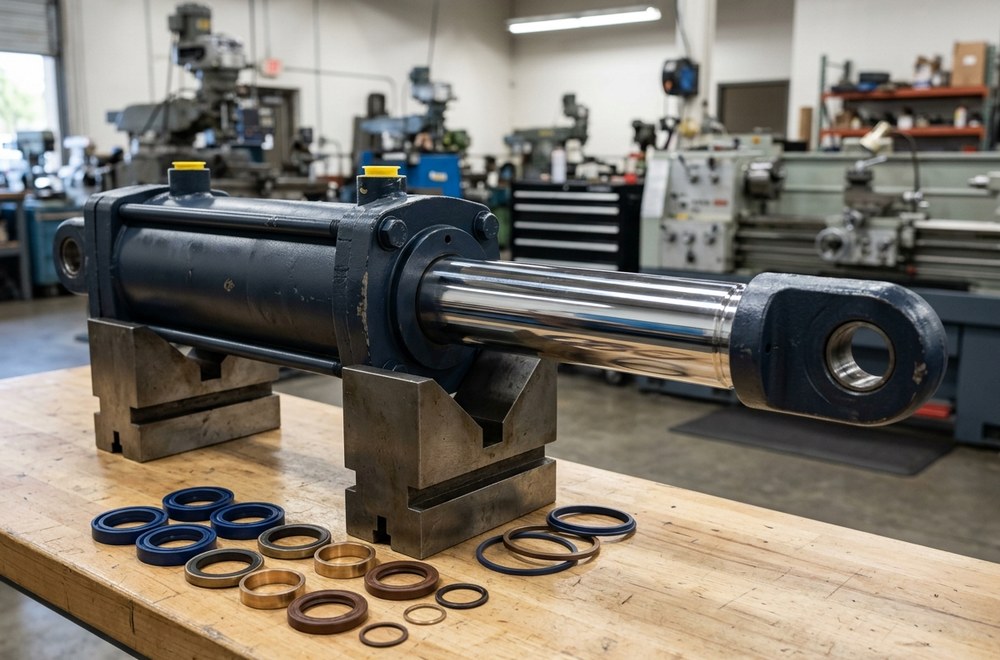
Scope
- Internal cylinder barrel bore honing and light machining
- Piston rod hard-chrome plating, micro-finishing, and straightening
- Installation of high-pressure marine polyurethane & PTFE seal kits
- Gland bronze bushing and piston guide band fabrication
- 350-bar hydrostatic pressure hold test, logged
How the job runs
- 1
Teardown & Rod Survey
Inspection for scoring, seawater pitting, and axial runout.
- 2
Hard Chrome & Micro-Finish
Precision electro-plating and centerless grinding to OEM tolerance.
- 3
Tube Honing
Bore cross-hatch honing for optimal seal lubrication and lifespan.
- 4
Seal Fitting
Marine-grade glycol/oil compatible high-temperature seal kit fitment.
- 5
350 Bar Pressure Hold
Hydrostatic test bench hold for 2 hours with zero pressure drop.
Equipment we work onRepresentative
- Hatch cover operating and lift cylinders (MacGregor, TTS, etc.)
- Steering gear rams and rotary actuator units
- Ro-Ro bow/stern ramp and car-deck cylinders
- Accommodation ladder and crane luffing rams
This list is representative. Send us your engine model and we will confirm the scope. Not an OEM authorisation.
Work in this service
Related guide articles
Questions
Can deeply scored hydraulic piston rods be salvaged?
Yes, by peeling the damaged surface, applying specialized sub-plating, hard chrome plating, and precision grinding back to OEM Ra 0.2 finish.
How are cylinders tested?
Every reconditioned cylinder undergoes a multi-hour 300+ bar pressure hold test, with results logged in the final inspection document.
Quote for this job
Tell us where the ship is and what failed; we'll review the scope and get back to you.